- Hygiene & Safety: Create non-porous, easy-to-clean surfaces that prevent bacteria buildup and contamination.
- Durability: Resist corrosion, chemicals, and wear from harsh food processing conditions.
- Regulatory Compliance: Meet FDA and industry food safety standards to ensure full compliance.
- Operational Efficiency: Reduce maintenance downtime and extend equipment lifespan.
- Versatile Applications: Ideal for equipment, surfaces, and storage in all types of food manufacturing facilities.
Industrial Food Grade Coatings – Why They Matter
In the fast-paced world of food manufacturing, maintaining the highest standards of hygiene, safety, and operational efficiency is crucial. One of the most effective ways to achieve this is through the use of Industrial Food Grade Coatings. These specialized coatings are designed to protect surfaces, prevent contamination, and ensure compliance with food safety regulations, helping you maintain a clean, efficient, and compliant manufacturing environment.
What are Industrial Food Grade Coatings?
Industrial Food Grade Coatings are protective layers applied to equipment, machinery, and surfaces in food processing facilities. These coatings are specifically formulated to meet the rigorous health and safety standards of the food industry, ensuring they won’t contaminate food products while providing superior durability, ease of cleaning, and protection against corrosion.
How Do Industrial Food Grade Coatings Work?
Food grade coatings create a non-porous barrier that resists food acids, oils, and moisture while offering superior protection against bacteria growth. Here’s how they enhance your food manufacturing operations:
✅ Enhanced Hygiene: The smooth, easy-to-clean surface minimizes bacteria buildup and ensures your equipment remains sanitary at all times.
✅ Corrosion Resistance: These coatings protect surfaces from rust and corrosion, which is especially important in high-moisture environments common in food processing.
✅ Chemical Resistance: Designed to withstand food-based acids, oils, and cleaning agents, food-grade coatings ensure long-lasting protection against harsh conditions.
✅ Compliance with Food Safety Standards: Industrial Food Grade Coatings meet or exceed FDA and other regulatory requirements, ensuring that your facility complies with the latest health and safety regulations.
Key Applications of Industrial Food Grade Coatings
🔹 Food Processing Equipment: Coatings are applied to mixers, conveyors, and storage tanks to ensure they stay safe and easy to clean without compromising food safety.
🔹Production Lines: Machinery used in the production of packaged foods, beverages, and dairy products is coated to protect against contamination and wear.
🔹Surfaces and Floors: Floors, walls, and ceilings in food manufacturing units are coated with food-grade materials to create easy-to-maintain, non-porous surfaces.
🔹Storage and Transport Equipment: Pallets, containers, and transport equipment benefit from food-grade coatings to ensure food safety during storage and shipment.
Industrial Food Grade Coatings vs. Regular Coatings
Feature | Regular Coatings | Industrial Food Grade Coatings
Food Safety Compliance | ❌ No | ✅ Yes
Hygienic Properties | ❌ Limited | ✅ High
Hygiene StandardsDurability |✅ Moderate |✅ High (resistant to harsh food processing conditions)
Corrosion Resistance | ❌ Low | ✅ Excellent in moisture-rich environments
Ease of Cleaning | ❌ Difficult | ✅ Smooth, easy-to-clean surfaces
Regulatory Compliance | ❌ No | ✅ FDA and industry-approved
Why Industrial Food Grade Coatings are Essential for Food Manufacturing
- Maintains Hygiene Standards: In food production, hygiene is non-negotiable. Industrial food grade coatings reduce the risk of contamination by preventing bacteria growth, ensuring that your facility meets the highest sanitation standards.
- Boosts Equipment Lifespan: These coatings protect your equipment from wear, corrosion, and damage caused by food acids and cleaning agents, significantly extending the life of your machinery.
- Ensures Regulatory Compliance: Adhering to strict food safety standards is critical in today’s industry. Food grade coatings meet FDA regulations and help you stay compliant with health and safety laws.
- Reduces Operational Downtime: The durability and easy-to-clean properties of food-grade coatings help reduce maintenance time, increasing overall production efficiency and minimizing costly downtime.
- Cost-Effective: By protecting your equipment and surfaces, industrial food grade coatings reduce the need for expensive repairs and replacements, making them a smart, long-term investment.
Frequently Asked Questions (FAQs)
1. How long do Industrial Food Grade Coatings last?
Food grade coatings are engineered for durability and can last several years with proper maintenance, providing long-term protection against corrosion, abrasion, and food-related chemicals.
2. Are Industrial Food Grade Coatings safe for all types of food processing?
Yes, these coatings are versatile and suitable for all types of food processing, including dairy, meat, bakery, beverages, and packaged goods.
3. Can food-grade coatings withstand frequent cleaning?
Absolutely! Food-grade coatings are designed to handle frequent cleaning and sanitization, making them ideal for the rigorous hygiene requirements of food manufacturing facilities.
4. How are these coatings applied?
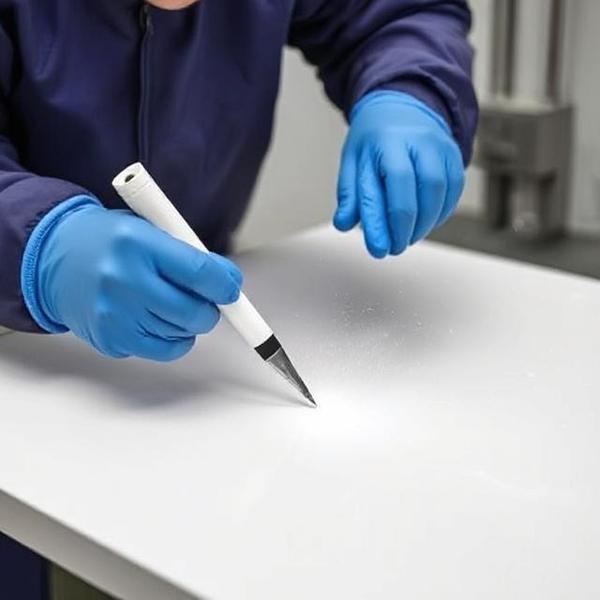
Industrial food grade coatings are typically applied through spray, brush, or roll-on methods, depending on the surface and equipment. The application is straightforward, with minimal disruption to operations.
Final Thoughts: Elevate Your Food Manufacturing with Industrial Food Grade Coatings
Ensuring a clean, safe, and efficient food manufacturing environment is crucial in today’s competitive and regulated market. Industrial Food Grade Coatings are a reliable, cost-effective solution to protect your equipment, prevent contamination, and maintain compliance with food safety standards. Whether you’re looking to extend the lifespan of your equipment or streamline your cleaning processes, these coatings are an essential investment for any modern food manufacturing facility.
🔹 Ready to safeguard your operations with high-performance food-grade coatings? Explore our range of Industrial Food Grade Coatings and transform your production environment today! 🚀
🔗 Related Reads:
✔️ The Importance of Compliance in Food Manufacturing
✔️ How to Choose the Right Coating for Food Processing Equipment
✔️ Top Challenges in Food Manufacturing and How Coatings Can Solve them.
coating food grade
coating food industry
coating in manufacturing
epoxy coating food grade
epoxy food grade coating
food coating ingredients
food coating pdf
food coating process
food grade ceramic coating
food grade coating
food grade coating for metal
food grade coating for plastic
food grade coating for stainless steel
food grade coating for water tanks
food grade coatings for metal
food grade epoxy paint manufacturers in india
food grade metal coatings
food grade powder coating
food grade teflon coating
industrial food coating machine
industrial food grade coatings for manufacturing units as per is code
industrial food grade coatings for manufacturing units bangalore
industrial food grade coatings for manufacturing units company in india
industrial food grade coatings for manufacturing units near me
Keywords